
In the field of electric drive manufacturing, laser welding of ultra-thin copper bars is a very challenging process. The seemingly simple copper bus welding actually has extremely high requirements on process accuracy and parameter control.
This article focuses on the inverter TPAK copper bar laser stack welding technology and comprehensively analyzes its process difficulties and technical implementation solutions.
TPAK: The core interconnection structure of the inverter
TPAK is an interconnection solution based on advanced power module packaging concepts. Its core structure uses an ultra-thin copper bar laser stack welding process to achieve electrical connections.
As the key path for power chip current derivation, the copper bar plays an important role in large current transmission. Its welding quality directly determines the reliability and safety of the electronic control system. Therefore, welding seam forming must achieve micron-level precision control.
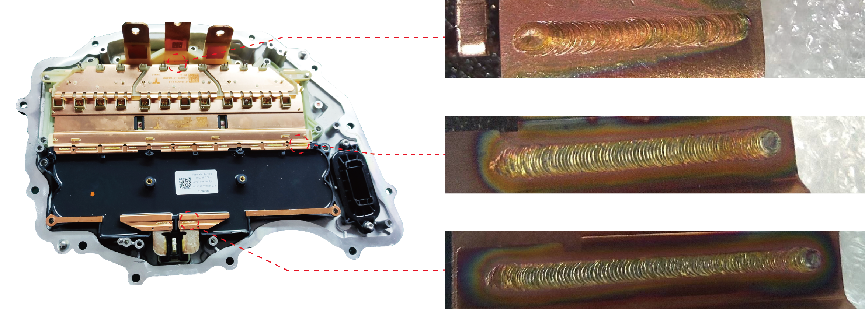
1.1 Inverter welding sample
This technical research focuses on the most difficult specification in the series - ultra-thin stack welding applications with a single-layer copper bar thickness of only 0.4mm.
Three major technical difficulties in welding 0.4mm ultra-thin copper bars
The thickness of 0.4mm is approximately equivalent to the stacking of 4 standard A4 papers. Under this thickness condition, stable stack welding can be achieved, and the process window is extremely narrow.
1. Strict requirements for heat input accuracy
Even if the laser power deviation is small, it may lead to welding failure: too high power will cause excessive penetration and damage the underlying insulation board; if the power is insufficient, the bonding strength of the two layers of copper bars will not be enough to meet the mechanical performance requirements. Therefore, this places extremely high requirements on equipment stability and process control accuracy.
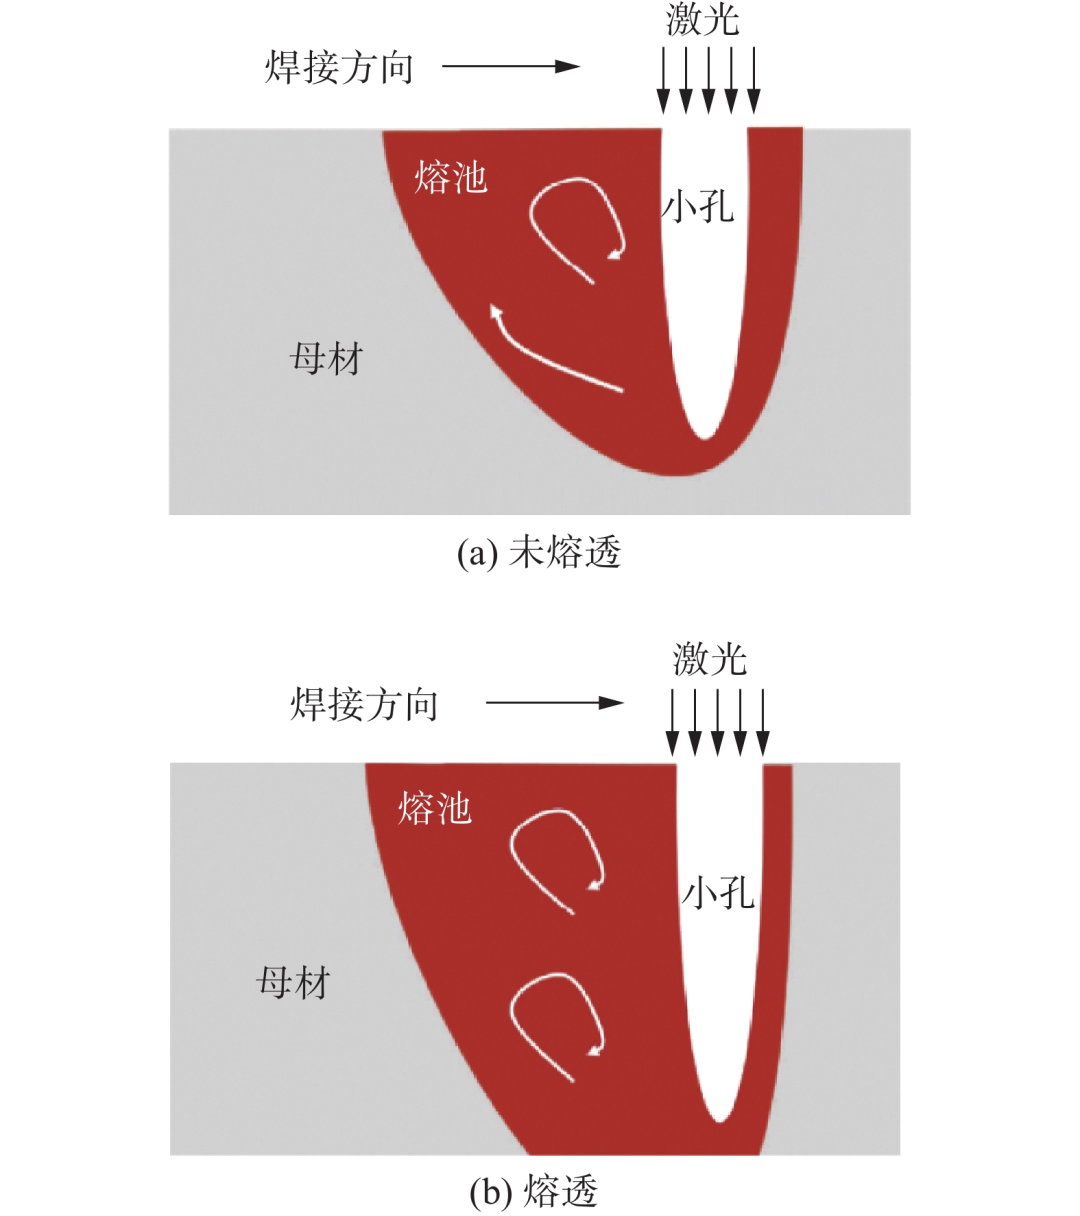
2.1 Cross-section diagram of laser welding in incomplete and full penetration states
2. It is difficult to control thermal deformation
Copper itself has the characteristics of high thermal conductivity and low hardness. The huge temperature gradient generated during the laser welding process will form significant thermal stress, which can easily cause warping and deformation of the copper bar. Even a deformation deviation of 0.1mm will have a serious impact on subsequent electrical performance.
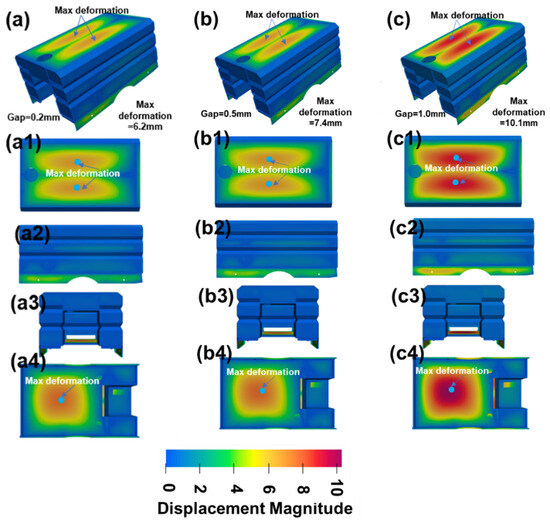
2.2 Displacement and deformation cloud diagram of thin plate welding under different working conditions
3. Narrow heat input
The stack welding process requires the upper copper bar to be completely penetrated and the lower copper bar to form a strong metallurgical bond. At the same time, the heat affected range must be strictly controlled. It is necessary to effectively prevent heat conduction from damaging the surrounding single-tube chips, and at the same time, completely protect the reflow soldering coating on the single-tube connection surface. Therefore, penetration control must be precise and controllable to ensure welding strength without damaging the underlying functional coating and surrounding sensitive devices.
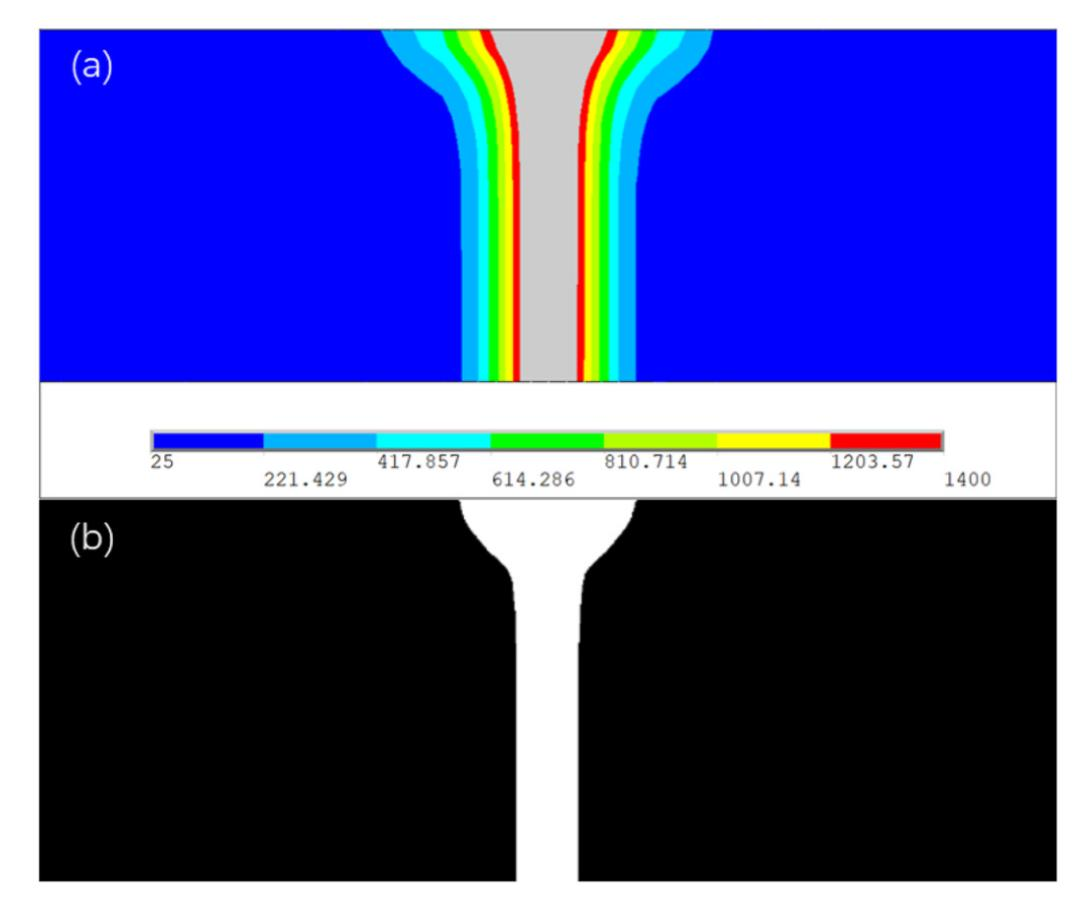
2.3 Temperature field cloud diagram of weld section
Spatter: The insurmountable quality red line of TPAK welding
If thin plate deformation is a process problem, then welding spatter is an absolute quality red line.
During the conventional laser welding process, tiny copper droplets are ejected from the molten pool due to the recoil force of metal vapor. After cooling, they form granular splashes that adhere to the surface of the workpiece.
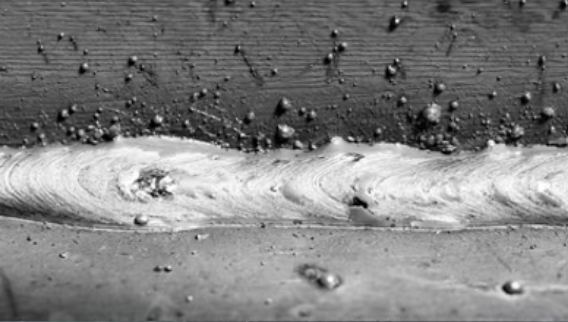
3.1.1 Large amounts of surface splash
3.1.2 Standard finished welds
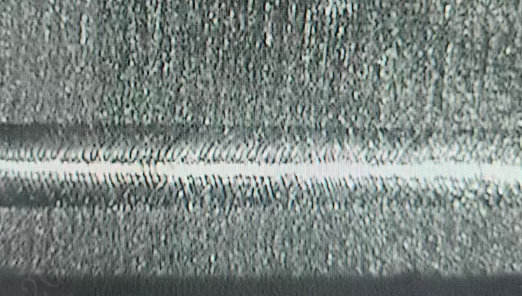
In TPAK products, solder joints with spatter are considered defective products. Copper particles generated by splashing have the risk of falling off in the long-term vibration operating environment of electric drives: copper particles with a diameter of 0.2mm falling off to the circuit board may cause a short circuit, and entering the insulation gap may cause creepage breakdown. The safety of electric drive systems does not allow for any potential risks, so a reasonable quality standard is zero splash, not reduced splash levels.
Laser welding: the optimal process choice for ultra-thin copper bars
In view of the process requirements of 0.4mm ultra-thin copper strip stack welding, the industry has carried out systematic comparative verification of various welding solutions:
Brazing: The heat affected zone is large and the deformation of the thin plate is difficult to control;
Resistance welding: The electrode pressure can easily cause the 0.4mm copper sheet to collapse, and the nugget size control accuracy is insufficient;
Ultrasonic welding: It has extremely high requirements on the surface condition of the workpiece and the accuracy of the tooling, and it is difficult to ensure the consistency of large-area overlapping welding.
None of the above processes can simultaneously meet the three core requirements of narrow heat input, micron-level penetration control and zero spatter.
Laser welding has become the preferred solution due to its unique advantages: energy can be focused to a spot of tens of microns, and the heating area can be precisely controlled; heat input can be finely adjusted at the millisecond level; non-contact processing does not have the problem of electrode loss.
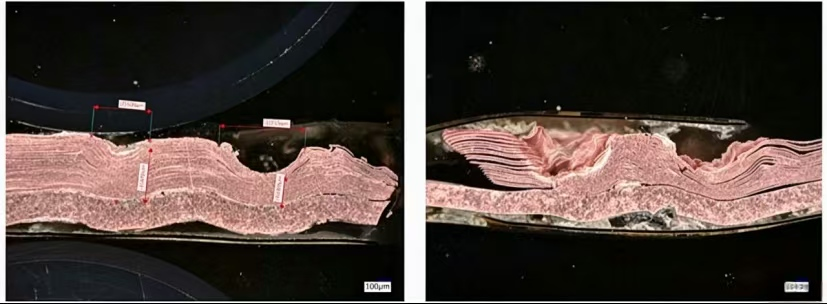
4.1 Copper foil under ultrasonic welding
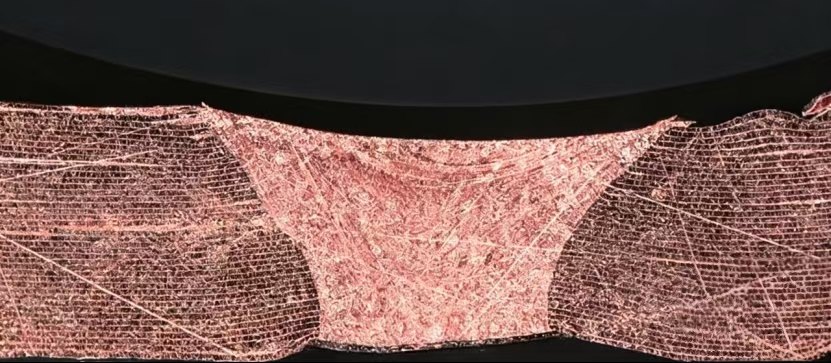
4.2 Copper foil after laser welding
Laser technology provides a feasible technical path for welding 0.4mm ultra-thin copper bars, but practical applications still face fundamental challenges caused by the high reflectivity of copper.
Physical contradictions of infrared laser welding of copper
The initial absorption rate of copper for commonly used infrared lasers (wavelength about 1065nm) is less than 5%. This physical characteristic brings two major problems to laser welding:
1. The molten pool is unstable
A large amount of laser energy is reflected by the copper surface, which not only causes energy waste, but also causes laser output power to fluctuate, causing the molten pool to be unstable and produce a large amount of spatter.
2. Heat input is difficult to accurately control
To overcome the problem of high reflectivity, it is usually necessary to increase the laser power. However, the absorption rate will rise sharply after the copper material is melted. The excessive energy injected instantly causes the molten pool to boil violently, making the spatter problem more serious. It is impossible to control the penetration depth of the 0.4mm thin plate.
This creates a technical contradiction: TPAK welding requires zero spatter and precise control of penetration, while the physical characteristics of ordinary infrared laser welding of copper are high reflection, high spatter, and difficult to control penetration. This is also the fundamental reason why "thin copper laser welding" has become a common technical difficulty in the industry.
Red and blue composite laser: breaking through technical bottlenecks from the principle level
Aiming at the inherent technical bottleneck of infrared laser welding of copper materials, red and blue composite laser welding technology can break through the process limitations caused by high reflectivity from the perspective of physical principles.
The core principle is that the absorption rate of blue laser (wavelength about 450nm) by copper can reach more than 65%, which is more than ten times that of the infrared band.
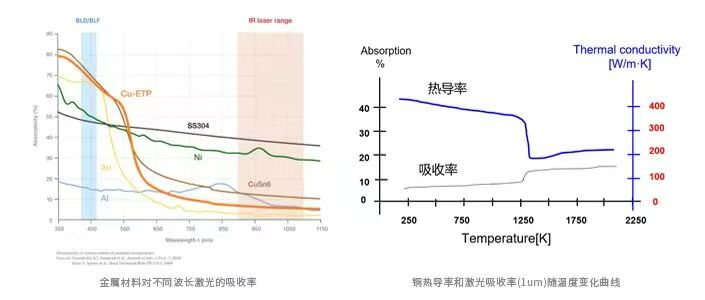
6.1 Changes in laser absorption rate
Based on this physical property, blue light can first achieve stable melting of the copper surface and establish a stable liquid molten pool; then infrared laser injects energy through the stable molten pool channel to complete deep penetration welding. During the entire process, the molten pool is always under the stabilizing effect of blue light, the keyhole fluctuations are greatly reduced, and the spatter suppression rate can reach more than 90%. At the same time, the energy input process is more controllable, and the penetration window of the 0.4mm copper bar can be accurately controlled.
This technical principle is the core support for achieving zero spatter and high-strength welding effects of ultra-thin copper bars. The microscopic action principle of red and blue composite laser and the deep mechanism of spatter suppression will be further analyzed in the following content.
About Zhongke Yichuang
Zhongke Yichuang (Guangzhou) Technology Co., Ltd. was incubated and established by the Greater Bay Area Integrated Circuit Research Institute. It is a key investment incubation project of the Chinese Academy of Sciences and has received key support from the Guangdong Provincial and Municipal Governments. The company has won many honors such as National High-tech Enterprise, Guangdong Province Specialized and New Enterprise, and Guangdong Province Top 100 Hard Technology Enterprises.
Currently, Zhongke Yichuang has its Guangzhou headquarters, Wuxi manufacturing base, Shanghai branch and Wuhan delivery center. The company focuses on the development of power bricks, motor controllers and domain controllers in the field of new energy vehicles. It not only obtained the first ASIL-D SiC motor controller product certification in China, but also passed many authoritative vehicle-level qualification certifications such as IATF16949, ASPICE L2, ISO9001, etc., showing strong system strength. In addition, the company has a complete set of capabilities in software, hardware, structure, testing, production and manufacturing, and has been recognized and praised by many OEMs.
Service support email:support@e-tronic.com.cn

Scan the QR code to follow丨E-tronic

